

Dimensional Inspection for Made-to-Print Parts
Dimensional inspection links a product definition given at the time of a product release to measurements made and an agreed upon acceptance decision. For a precision part, design, quality and procurement teams need to specify the characteristic, method, part condition, sampling and report before production begins.
Compare Inspection Methods
- Product definition
- Feature & datum
- Method & traceability
- Part state & points
- Lot sampling
- Decision & record
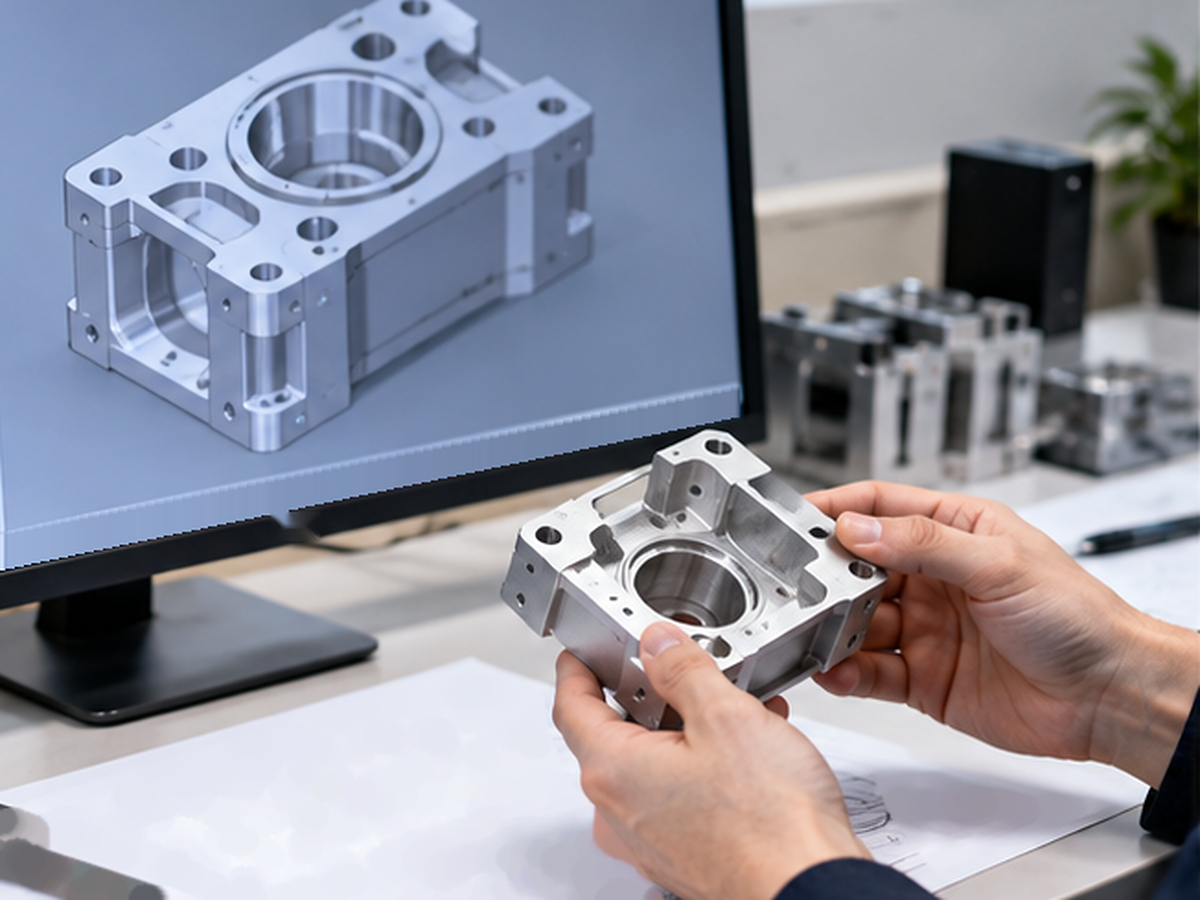
Commercial handoff at a glance
Quote review
1–3 business days
Quotes are returned within 1–3 business days, reviewed by an engineer.
Prototype
7–14 business days
Prototype parts ship in 7–14 business days after drawing approval.
Small batch
2–3 weeks
Small-batch orders ship in 2–3 weeks after drawing approval.
Production
3–6 weeks
Production runs are scheduled at 3–6 weeks, confirmed with your quotation.
Order scope
Project-based
Project-based; single-piece prototypes can be reviewed.
Files
Model + drawing
We work from STEP or STP models paired with a dimensioned PDF drawing.
Measurement Capabilities and Equipment
No single instrument is best for every characteristic. A CMM is not always the quickest or clearest solution. Each method comes at a trade-off for feature, tolerance, datum scheme, access, surface, part size, flexibility, and the sort of record the customer requires.
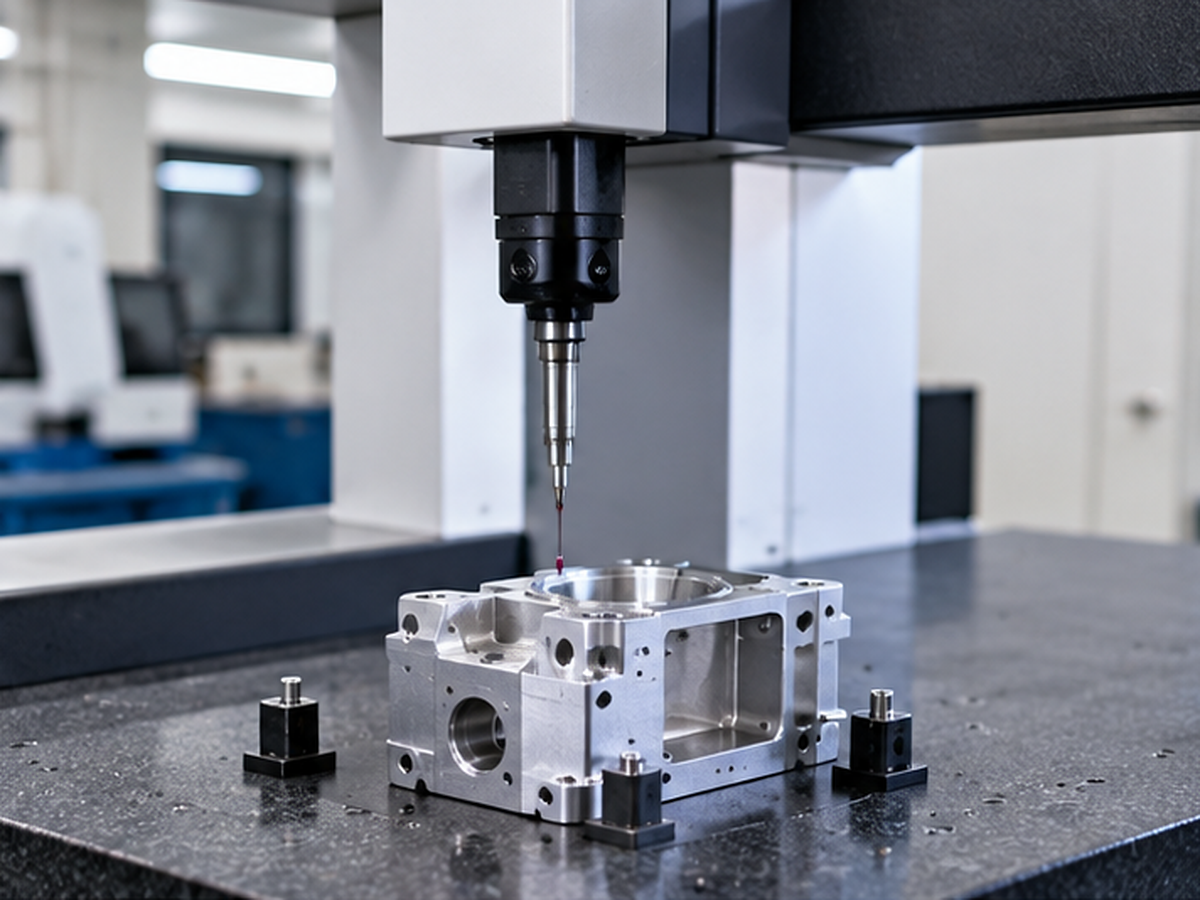
Inspection Methods
CMM Architecture
The mistake is choosing by machine name first. Fix the measurand and decision requirement, then compare viable methods.
| Method | Best suited for | Watch-outs | Record produced |
|---|---|---|---|
| Calipers and micrometers | Accessible sizes, thicknesses and diameters with direct contact | Operator technique, contact force, alignment and limited geometric context | Individual variable readings or attribute checks |
| Height gauge and surface-plate methods | Heights, steps, locations and comparative checks from a stable datum | Setup, part support and datum simulation | Feature readings tied to the stated setup |
| Coordinate measuring machine | Three-dimensional features, positions, profiles and datum-related geometry | Program, alignment, probe access, point strategy, fixturing and environment | Programmed dimensional record and feature results |
| Optical comparator, vision system or scanner | Small edges, non-contact evaluation and dense surface capture | Reflective or translucent surfaces, line of sight, edge definition and scan coverage | Image-based dimensions, profiles or surface datasets |
| Functional gauge | Fast verification of a defined assembly or envelope condition | Usually gives attribute evidence rather than a numerical result | Pass/fail or go/no-go record |
Coordinate systems matter. A CMM measures in its machine coordinate system, then relates the part coordinate system through datums or workpiece features.[4] That is why the alignment and characteristic definition belong in the inspection plan.
| Architecture or option | Useful question | Decision boundary |
|---|---|---|
| Bridge or gantry machine | Does the machine use air bearings, linear scales and computer control across the X, Y and Z axes? | Ask for the method behind any measurement accuracy or high precision statement; machine architecture alone does not establish a precise measurement or prove the requested precision target. |
| Horizontal arm CMM or arm CMM | Can the horizontal arm reach the required features on large parts without an unstable setup? | Access can improve while stiffness, alignment and the chosen probe system still govern the result. |
| Cantilever machine | Does open access suit the complex part and its fixture? | The machine envelope must still support the datum scheme, flatness evaluation and required uncertainty. |
| CMM software and probe system | How are design specifications, feature construction and point strategy translated into the program? | CMM technology supports a result only when the program and report preserve the released definition. |
| Laser scanning or laser scanner | Is dense contour capture needed for comparison or reverse engineering? | A scan can support geometry review without automatically proving that a part meets its acceptance requirements. |
Service scope comes before equipment labels. A CMM inspection service should connect the manufacturing process and design specifications to an agreed record; an inspection service is not just machine access. When comparing dimensional inspection services for an aerospace, automotive or medical device program, ask how CMMs use the released datum scheme and who applies the decision rule.
Inspection Method Selector
Compare candidate methods from geometry, access, surface, tolerance class and reporting need.
Open the selector →Brief before equipment
- Name the feature and datum.
- State the part condition.
- Define the required record.
Part Materials and Measurement Conditions
Zhenling manufactures made-to-print components in carbon and alloy steels, stainless steels, aluminium alloys and selected high-performance alloys. Having the name of the material alone is not sufficient for developing a measurement plan; flexibility, mass, surface condition and state of the part in addition to its thermal response are all important factors too.
Record the measurement temperature or stabilisation condition when thermal expansion could change the result. In the NIST length-metrology context, temperature measurement and control are among the contributors considered in dimensional uncertainty.[2]
Thin walls, bent tubes and compliant features can move under probing or clamping. Agree how the part will be supported and whether its free-state or restrained state governs.
Contact, reflected light and edge detection respond differently to machined, polished, coated or highly reflective surfaces. Treat surface preparation as a method-selection question for optical inspection, especially when reflection or edge definition may affect capture.[7]
Identify whether measurement occurs after rough machining, final machining, heat treatment, coating or assembly. The report should name the inspected state.
Surface Condition and Inspection Readiness
A controlled inspection condition establishes a clean reading. Burrs, chips, oil films, build-up, and lack of part temperature stability have the tendency to change either the physical feature or how the sensor perceives it.
-
REQ-01
Remove loose chips and handling contamination.
-
REQ-02
Identify burrs which are part defects as opposed to measurement artefacts.
-
REQ-03
Decide whether dimensions apply before or after plating, anodizing, or coating.
-
REQ-04
Allow the part and measurement environment to stabilise when required.
-
REQ-05
State the support, clamp or free-state condition.
-
REQ-06
Mark surfaces that are inaccessible or sensitive to contact.
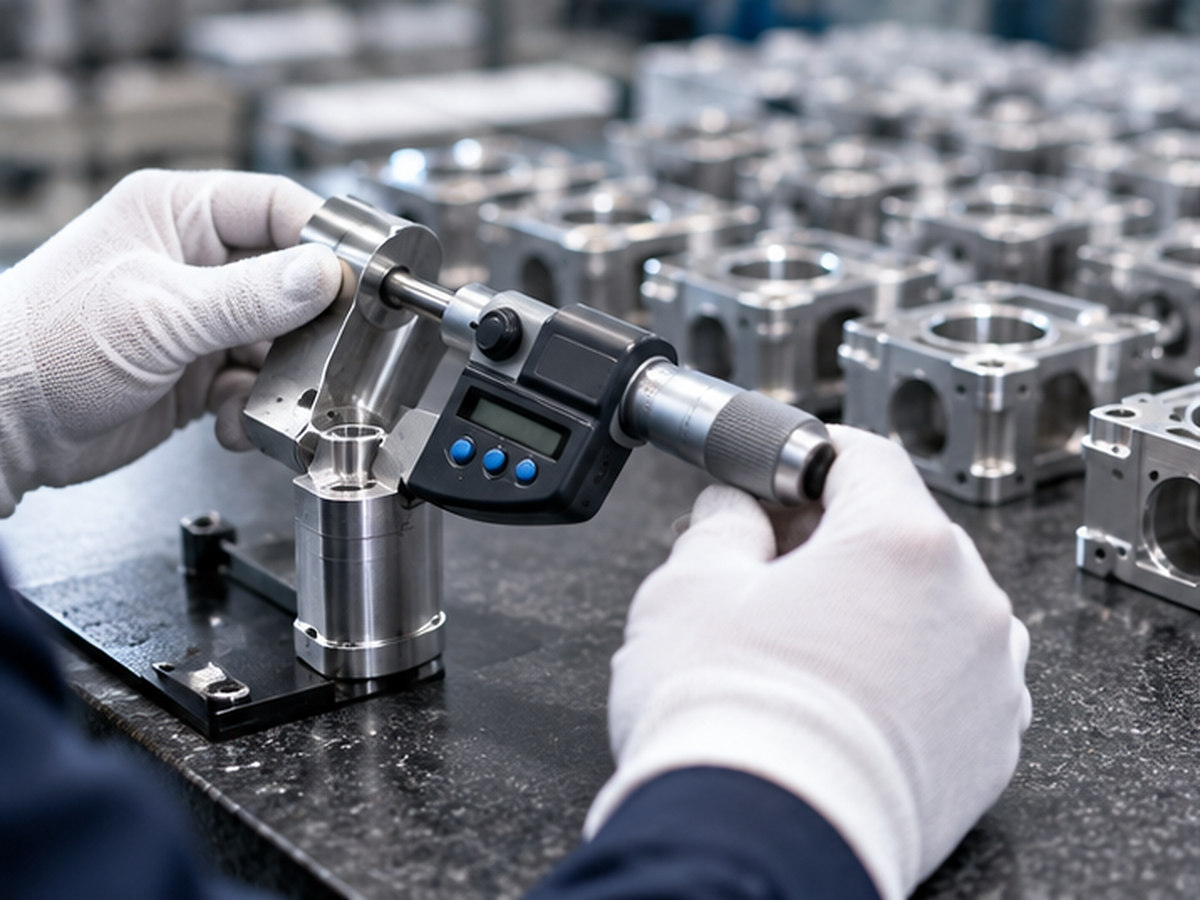
Example
the same bore can produce different inspection conversations if one party expects an uncoated machined size and the other measures after coating. Put the required state beside the characteristic before requesting the quotation.
Request Quotation State
Specifications & Metrology
Drawing Callouts, Tolerances and Report Scope
A useful inspection brief describes more than a nominal dimension. Although the tightest numerical specification may not always be the only driver, the measurement plan may be influenced by the relationship of the datum, part state, and the decision to be made.
Tolerance & Limit Converter
Calculate upper and lower limits for bilateral, unilateral or direct-limit inputs. The result is arithmetic support, not an acceptance decision.
Open the converter →Minimum input set
- Nominal and tolerance format
- Unit and drawing revision
- Feature and datum identifiers
- Part state and decision rule
Traceability Standards
Traceability belongs to the result. A calibrated instrument is not a substitute for result-level traceability. NIST describes an unbroken documented calibration chain in which each link contributes to uncertainty.[1]
Size limits
A bilateral tolerance creates limits above and below nominal; a unilateral tolerance moves in one direction. Limit dimensions state the permitted endpoints directly.
Datum relationship
Position, orientation, runout and profile results depend on the referenced datum system and alignment. A size result alone cannot substitute for that relationship.
Measurement capability
Instrument resolution is not the same as result uncertainty. Repeatability, reproducibility and other influences must be considered for the result and its intended use.[6]
Decision rule
State whether the deliverable is data only, an attribute result, or a conformity decision. This avoids treating every reported number as an automatic acceptance.
Worked dimensional-record example
The values below demonstrate how nominal, limits and actual results relate to a characteristic identifier. Real records use the released product definition and the project’s agreed decision rule.
| Feature ID | Characteristic | Nominal | Permitted limits | Example result |
|---|---|---|---|---|
| F01 | Outside diameter | 25.000 mm | 24.990–25.020 mm | 25.006 mm |
| F02 | Hole spacing | 60.000 mm | 59.950–60.050 mm | 60.018 mm |
| F03 | Perpendicularity | 0.000 mm | 0.080 mm max | 0.041 mm |
| F04 | Position tolerance | 0.000 mm | ⌀0.100 mm max | ⌀0.062 mm |
| F05 | Surface width | 32.000 mm | 31.980–32.020 mm | 31.991 mm |
| F06 | Included angle | 90.00° | 89.90–90.10° | 90.04° |
Inspection Scope, Pricing and Lead Times
Effort required for inspection will change depending on characteristic count, setup, program development, datum strategy, fixture requirements, access, sampling method, and report formatting. Send the released definition and critical-feature list so the quotation can separate manufacturing work from optional inspection documentation.
Cost drivers
- Number and type of characteristics
- New or reusable measurement program
- Fixture and support strategy
- Lot sample size and per-part point strategy
Report drivers
- Data-only or pass/fail output
- Selected features or full ballooned record
- First-article format
- Customer approval and revision loops
Schedule drivers
- Material and machining route
- Outside finishing
- Inspection programming and review
- Expedite feasibility
Process & Approval
Our handoff commitments: First-article approval and report scope are confirmed in the RFQ before production. Expedite requests are reviewed against material, capacity, finishing, and inspection scope before confirmation.
Documentation Scope
Your quotation itemises the actual inspection scope, delivery schedule and documentation. Project-specific review keeps price and timing connected to the released part definition.
Quality Control and Dimensional Records
Each measurement report documents its findings. The risk here is considering data and acceptance as equivalents because a conformity decision also relies on an agreed product definition, decision rule, responsibility and report scope.
Control the definition.
Bind the model, drawing, revision and characteristic list, then verify that the files agree.
Name the measurand.
Identify the feature, datum and required result.
Plan the method.
Document setup, equipment, result traceability, and relevant uncertainty.
Control the part state.
Define support, finish, temperature and per-feature point strategy.
Choose lot sampling.
State which units and how many parts are inspected.
Apply the decision rule.
Separate measurement data from pass/fail or release authority.
A credible result starts with a controlled definition and ends with a report whose decision boundary the buyer understands.
“Metrological traceability requires the establishment of an unbroken chain of calibrations to specified reference measurement standards.”
NIST Policy on Metrological Traceability[1]
Dimensional Report Anatomy
| Report field | What it should identify | Why the buyer needs it |
|---|---|---|
| Definition | Drawing/model number and revision | Prevents inspection against the wrong authority dataset |
| Part | Part number, lot, serial or sample identifier | Connects data to the physical item |
| Characteristic | Balloon or feature ID, datum and requirement | Shows exactly what was evaluated |
| Result | Nominal, limits, actual value, deviation and unit | Allows independent reading of the measurement |
| Method context | Method/equipment, setup, state and sampling | Explains how the value was obtained |
| Decision | Data only, attribute result, pass/fail and approval record | Prevents a measurement table from being mistaken for release authority |
Why scope must be explicit
In the report schema recommended on this page, attribute results and variable numerical data are separate fields, not interchangeable labels.
Keep the deliverables distinct
a certificate of conformance and a dimensional record are not interchangeable. Aerospace or automotive programs may impose customer-specific forms, so name the exact record and decision the receiving team needs.
Accredited-scope input
if an ISO/IEC 17025-accredited scope is a contract requirement, name the exact test or calibration activity in the RFQ and keep it separate from the part-acceptance decision.[8]
From Drawing Review to Inspection Release
-
STEP 01
RFQ input.
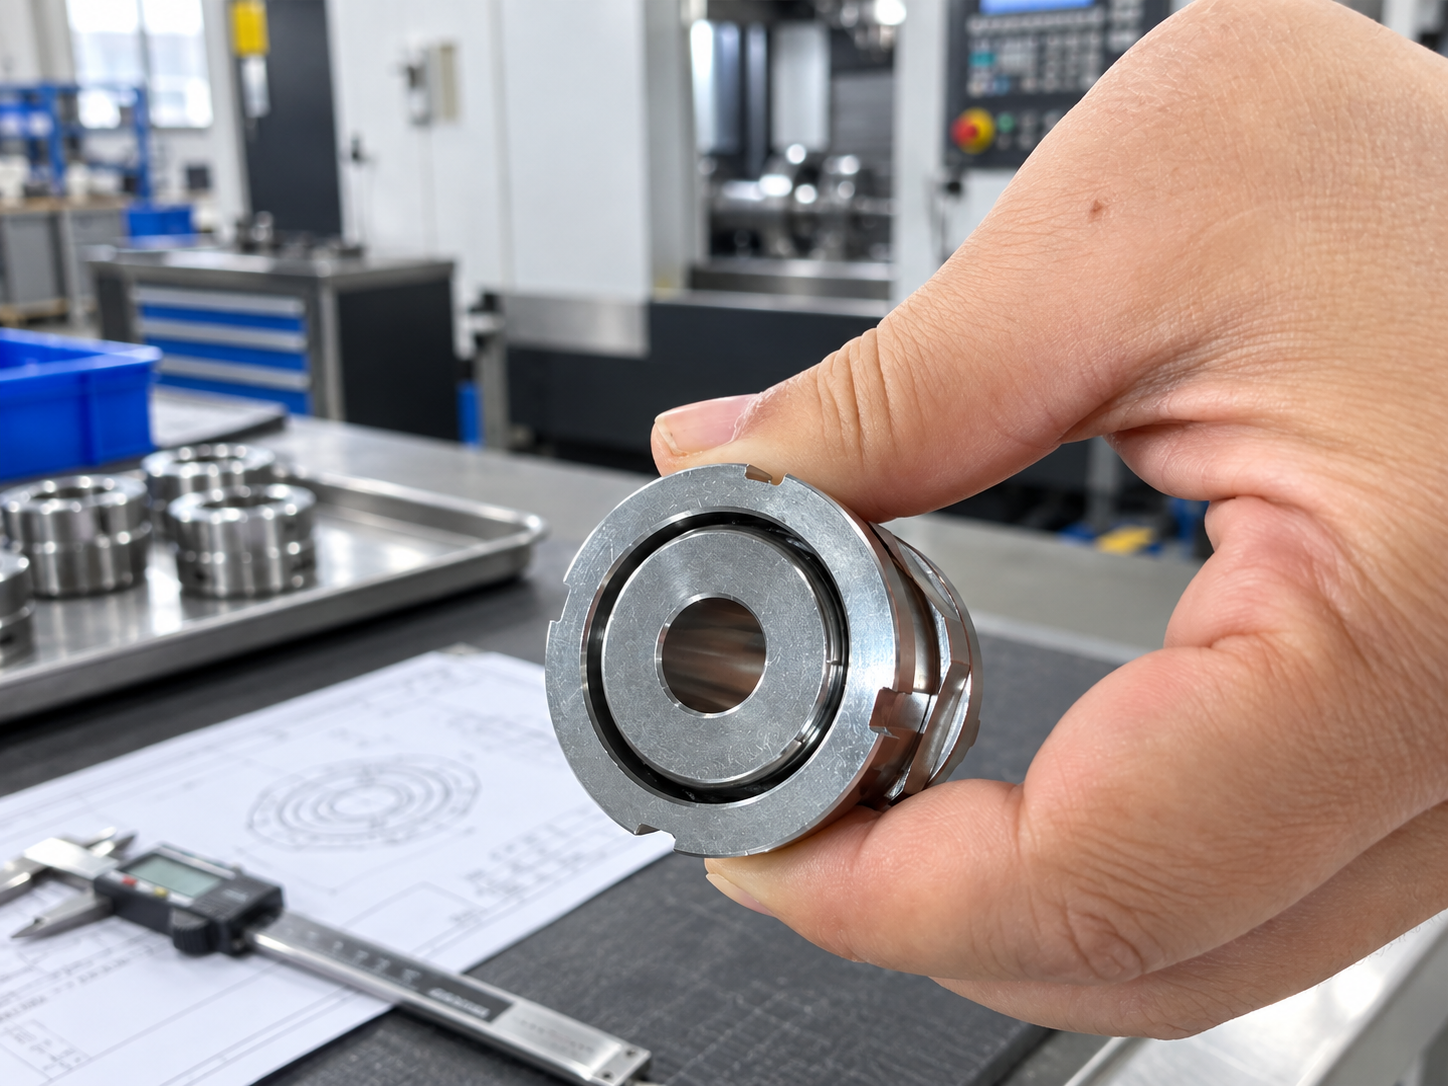
Send STEP or STP models paired with a dimensioned PDF drawing, quantity, material, finish and target date.
-
STEP 02
Definition review.
We identify: revision, critical characteristics, datum scheme, part state, and open questions.
-
STEP 03
Inspection plan.
The inspection plan contains consistent details for method, setup, feature coverage, point strategy, lot sampling and report format.
-
STEP 04
First article.
The agreed sample is measured before the production plan continues.
-
STEP 05
Production sampling.
Lot selection is performed independently of the number and distribution of points used to define each feature.
-
STEP 06
Record and release.
Agreed dimensional or first-article inspection records ship with your order.
Dimensional RFQ Checklist
Build a concise handoff list for files, characteristics, sampling, report scope and acceptance needs.
Confidential files
Your drawings are handled as confidential; an NDA can be reviewed before sensitive CAD files are shared.
Inspection Equipment in Our Facility
In 2006, Shanghai Zhenling Hardware Co., Ltd. was founded. Our Jiashan manufacturing site uses coordinate-measurement equipment for made-to-print component inspection.
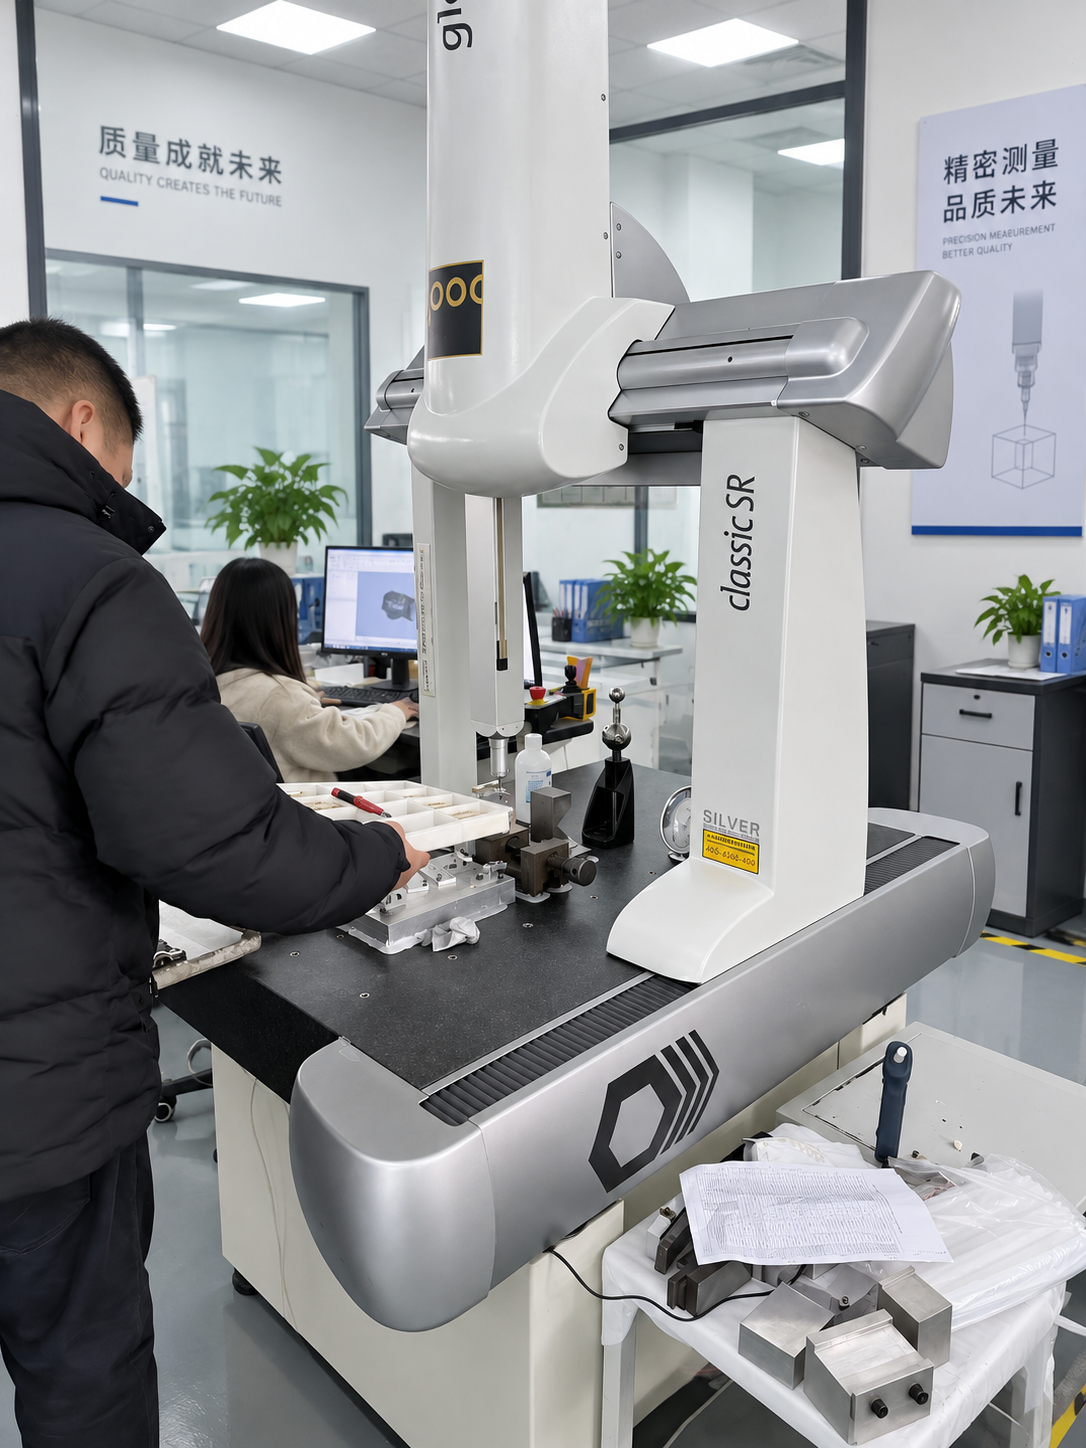
CMM UNIT // 01
Operator using a bridge coordinate measuring machine in Zhenling’s inspection area
Bridge coordinate measurement in a dedicated inspection area.
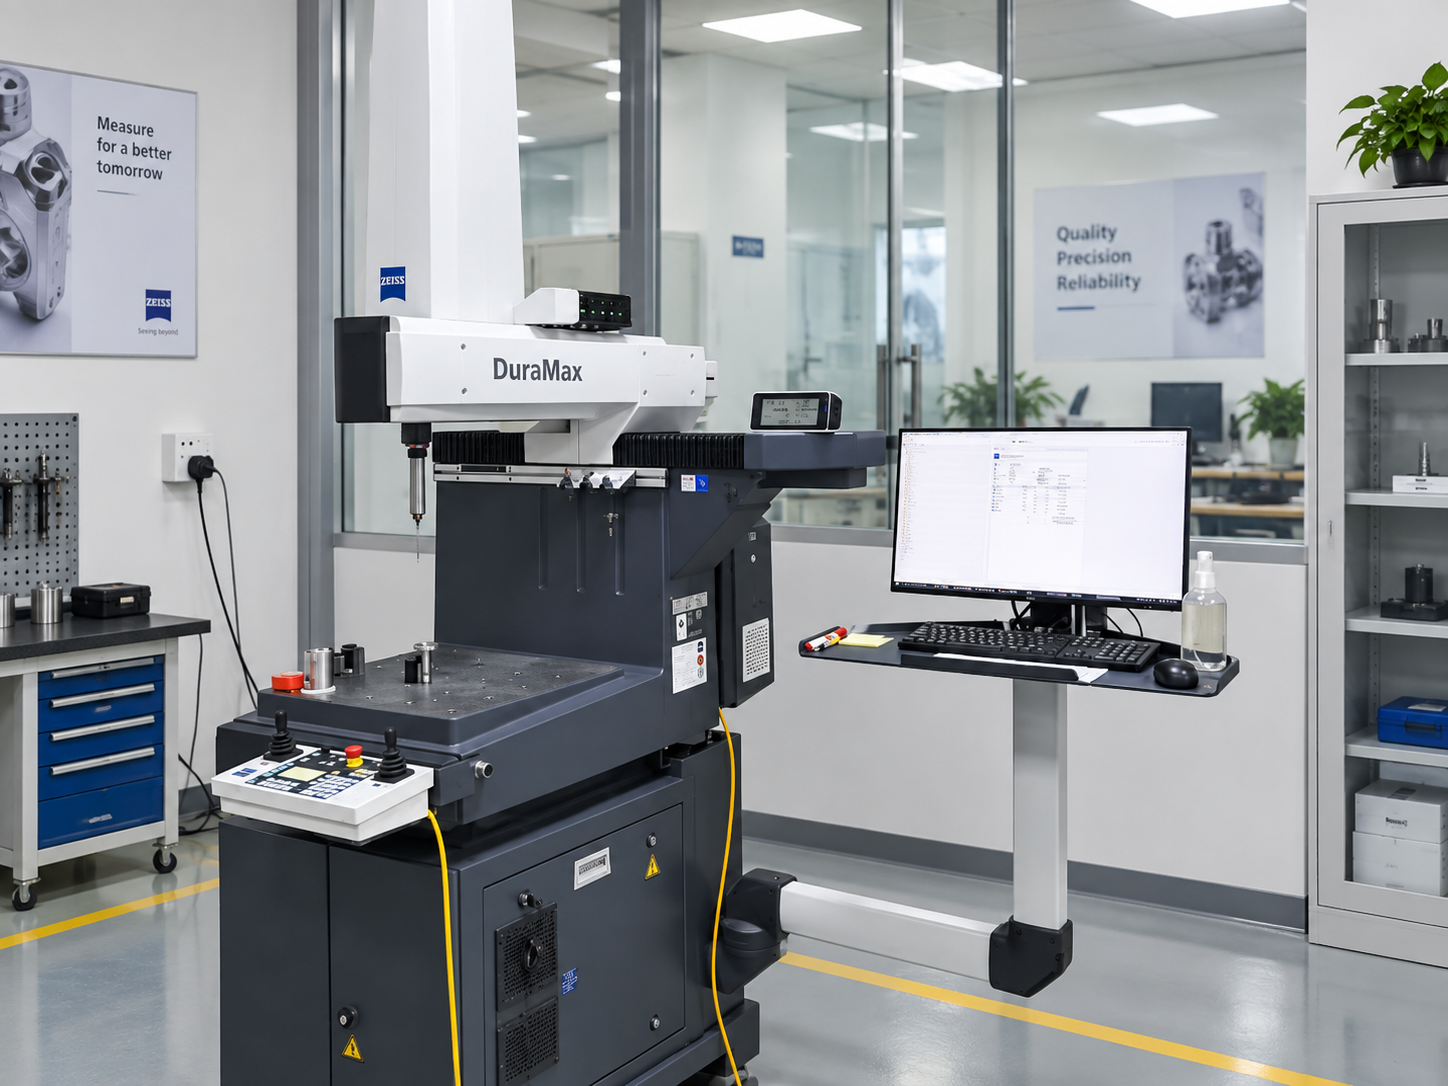
CMM UNIT // 02
ZEISS DuraMax coordinate measuring machine at Zhenling
ZEISS DuraMax equipment visible in the supplied facility photograph.
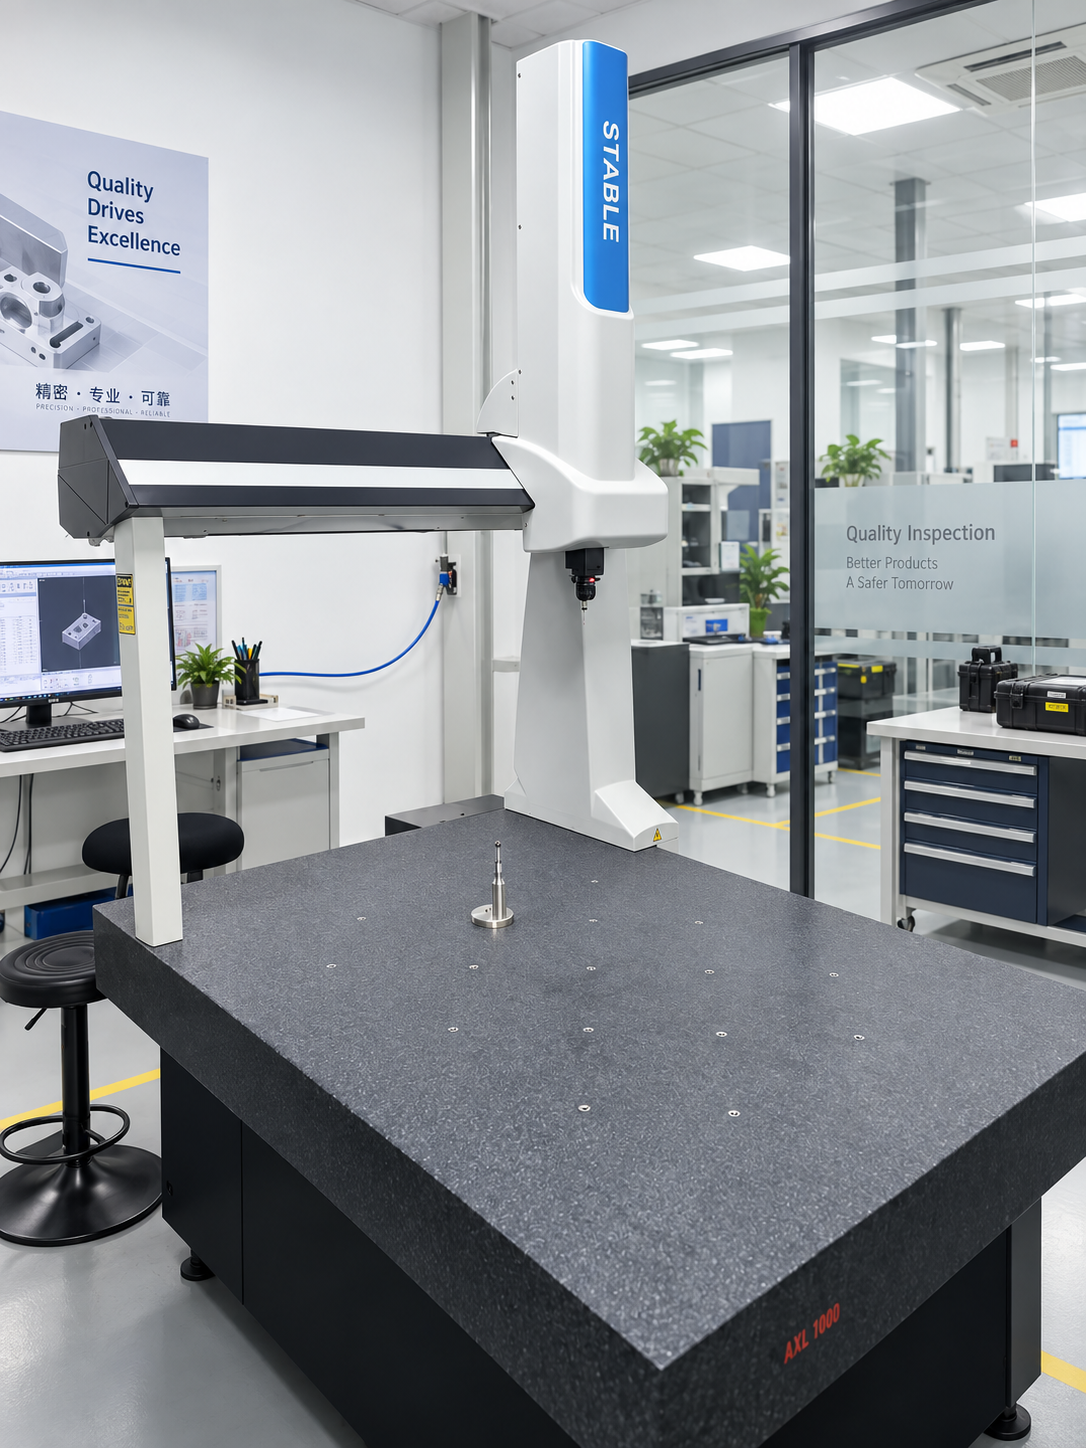
CMM UNIT // 03
Bridge coordinate measuring machine in the Zhenling facility
Bridge CMM in the inspection area; project suitability is confirmed during drawing review.
Project confirmation: the quotation and inspection plan connect each characteristic to feature access, setup, reporting and project-specific verification needs. Achievable performance is confirmed per feature during drawing review.
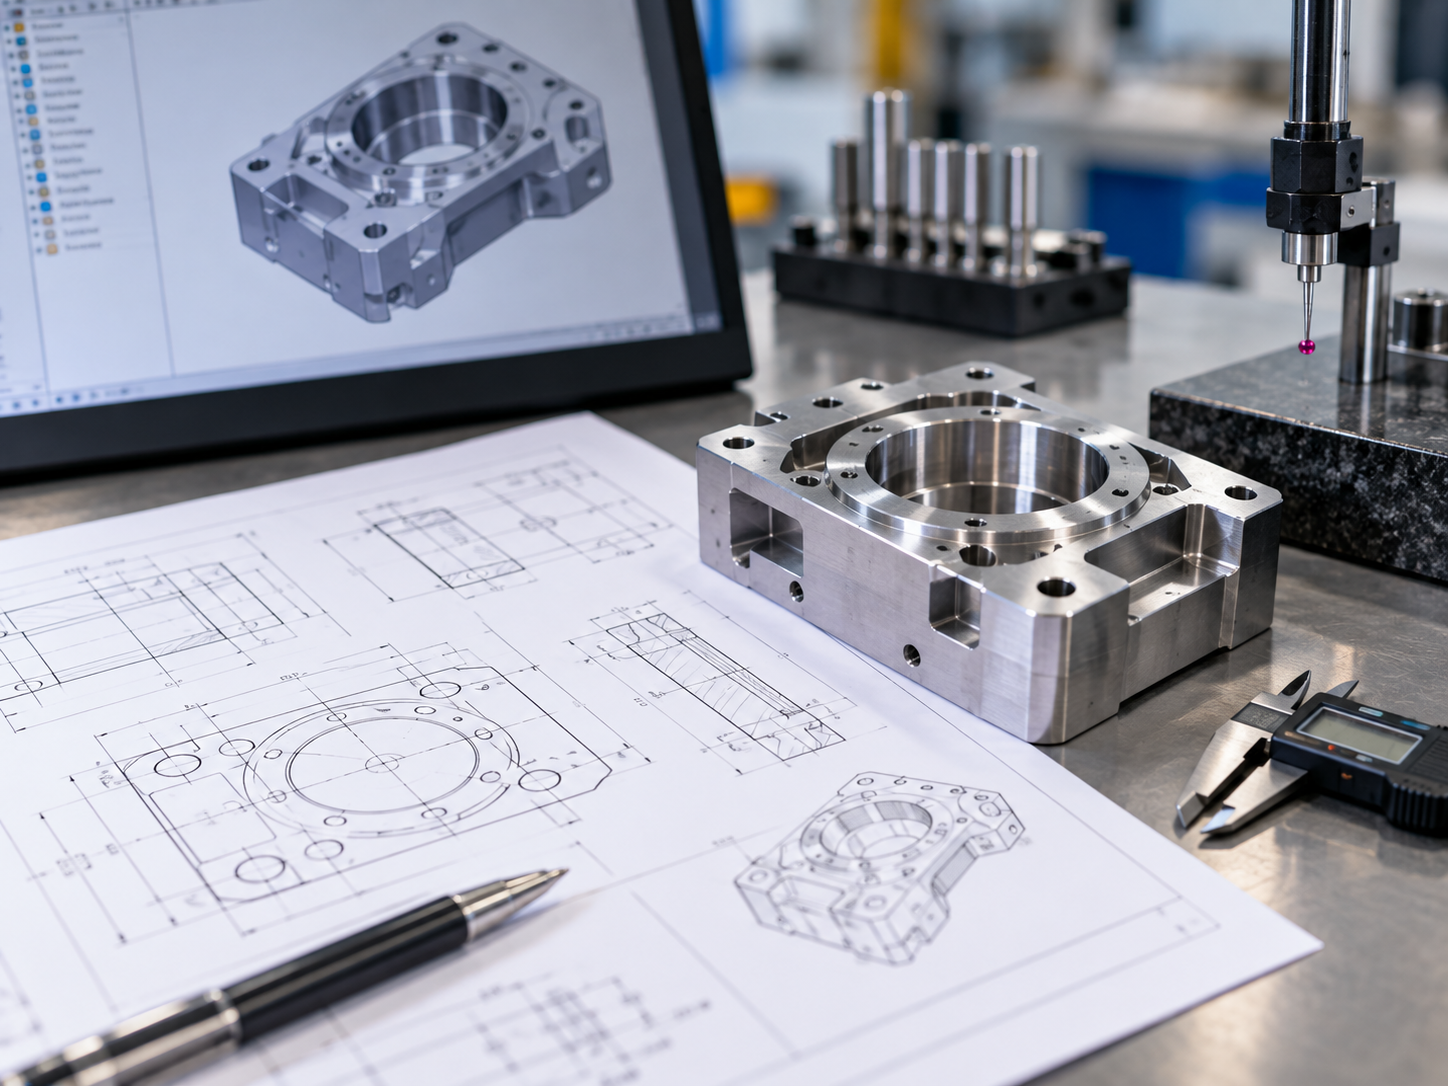
Where Each Measurement Method Reaches Its Limit
Hand tools
Fast for accessible size checks, but limited for complex datum relationships, freeform profiles and repeatable three-dimensional location.
CMM
Powerful for coordinate geometry, but probe access, alignment, fixturing, compliant parts and point distribution can limit the result.
Optical methods
Dense, non-contact capture can help with edges and surfaces, but reflectivity, transparency, line of sight and preparation can become constraints.[7]
Functional gauges
Efficient for a defined functional boundary, but often return an attribute result without the numerical data needed for process analysis.
External accredited laboratories or specialised testing may be appropriate when a contract requires a named accredited scope, an unavailable method, independent third-party reporting or measurement beyond the reviewed setup. If ISO/IEC 17025 accreditation is a contract requirement, identify the exact test or calibration scope rather than relying on a general accreditation statement.[8]
Escalation rule: when the method cannot support the feature, uncertainty need or acceptance record, change the plan before measuring. More data is not always better; select equipment only after the measurand and decision requirement are clear.
Dimensional Inspection Engineering Tools
Dimensional RFQ Checklist
Compile critical dimensions, tolerances, and GD&T requirements prior to manufacturing RFQ submission.
Tolerance & Limit Converter
Calculate arithmetic limits and tolerance ranges based on nominal dimensions and defined deviations.
Inspection Method Selector
Identify appropriate metrology equipment and inspection techniques based on part geometry and accuracy specifications.
Dimensional Inspection FAQs
What is dimensional inspection?
Dimensional inspection compares measurable part characteristics with a controlled product definition. A complete plan also identifies the datum, method, part condition, sampling, result record and any acceptance decision.
What should a dimensional inspection report include?
Include the product revision, part or lot identity, characteristic ID, nominal and limits, actual value, unit, method context, sampling and approval record. State whether the report is data only or includes pass/fail.
How should first-article and production sampling be specified?
Define the first-article unit and approval record, then separately define how many production units are sampled and when. For each characteristic, also define the measurement-point strategy where feature construction depends on sampled points.
How do temperature and part condition affect dimensional measurement?
Thermal expansion, support, clamping, surface condition and production state can change the part or the sensor interaction. Record the relevant condition and allow stabilisation when the tolerance and material make it necessary.
When is CMM inspection a better choice than calipers or micrometers?
A coordinate measuring machine is useful when the result depends on three-dimensional feature location, a datum reference frame, profile or repeated programmed evaluation. Direct hand tools can be more efficient for accessible sizes when their method and uncertainty are suitable.
Does an inspection report mean a part is accepted?
Not automatically. Acceptance requires the agreed requirement, decision rule and authority; a variable dimensional record can provide numerical measurements separately from an attribute pass/fail result.[5]
Which files should be sent for an inspection quotation?
Send the released STEP or STP model with a dimensioned PDF drawing, revision, material, finish, quantity and critical-characteristic list. Add the datum scheme, lot sampling, report format, acceptance requirement and target date.



