By XCX · Updated September 2026
First article vs first piece inspection is not a choice between two names for the same check. A machine shop may use first piece inspection to release a setup or defined production event, while first article inspection typically verifies product requirements rather than releasing the final product. Refer to the purchase document, drawing, quality clauses, control plan, contract, and applicable standard to clarify the intent and level of evidence required for validation.
Short answer
Use FAI when the governing requirement asks for documented verification of specified product characteristics and related records. Use a first-piece check when the applicable procedure asks for approval of the first unit from a setup, shift, lot, supplier change, restart, or other named event. The same physical part can sometimes support both records, but a quick setup check doesn’t become a complete FAI merely because it was performed on the first part.
1. Find the ownerContract, drawing, standard, or control plan
2. Define the decisionProduct verification, setup release, or another approval
3. Match the evidenceCoverage, actual results, traceability, and approval
First article vs first piece inspection: the short answer
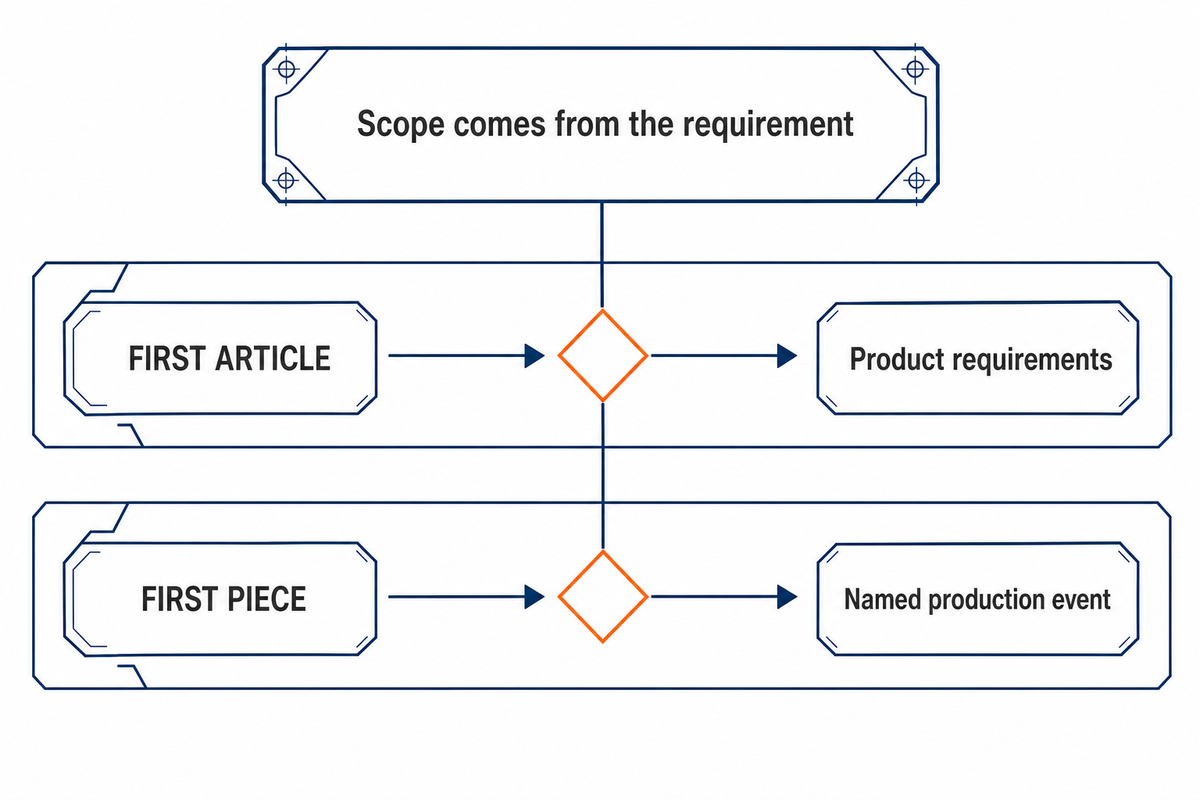
A first article inspection commonly asks whether the first production output made by the planned methods conforms to the defined product requirements. Its evidence can include drawing-characteristic results, revision identity, materials or special-process references, traceability, nonconformance disposition, and approval records, depending on the controlling requirement.
Evidence: FAR Subpart 9.3.
| Decision field | First article inspection | First piece inspection |
|---|---|---|
| Common purpose | Document product verification for a new or changed requirement | Release a defined production event before work continues |
| Possible trigger | New part, revision, source/process change, lapse, or customer flow-down | Setup, tool/program/fixture change, shift, lot, supplier, restart, or another procedural event |
| Typical evidence depth | Broader characteristic and documentation package | Evidence needed to support the event-specific release decision |
| Authority | Customer, contract, standard, or internal quality procedure | Customer, control plan, work instruction, or internal quality procedure |
A first piece inspection may also be issued for setup evaluation. It typically focuses on determining whether a defined shift, setup, production lot, program state, or sourcing event may proceed. Evidence for first piece inspection follows the governing procedure and may include setup-sensitive process controls or other named characteristics.
What is first article inspection?
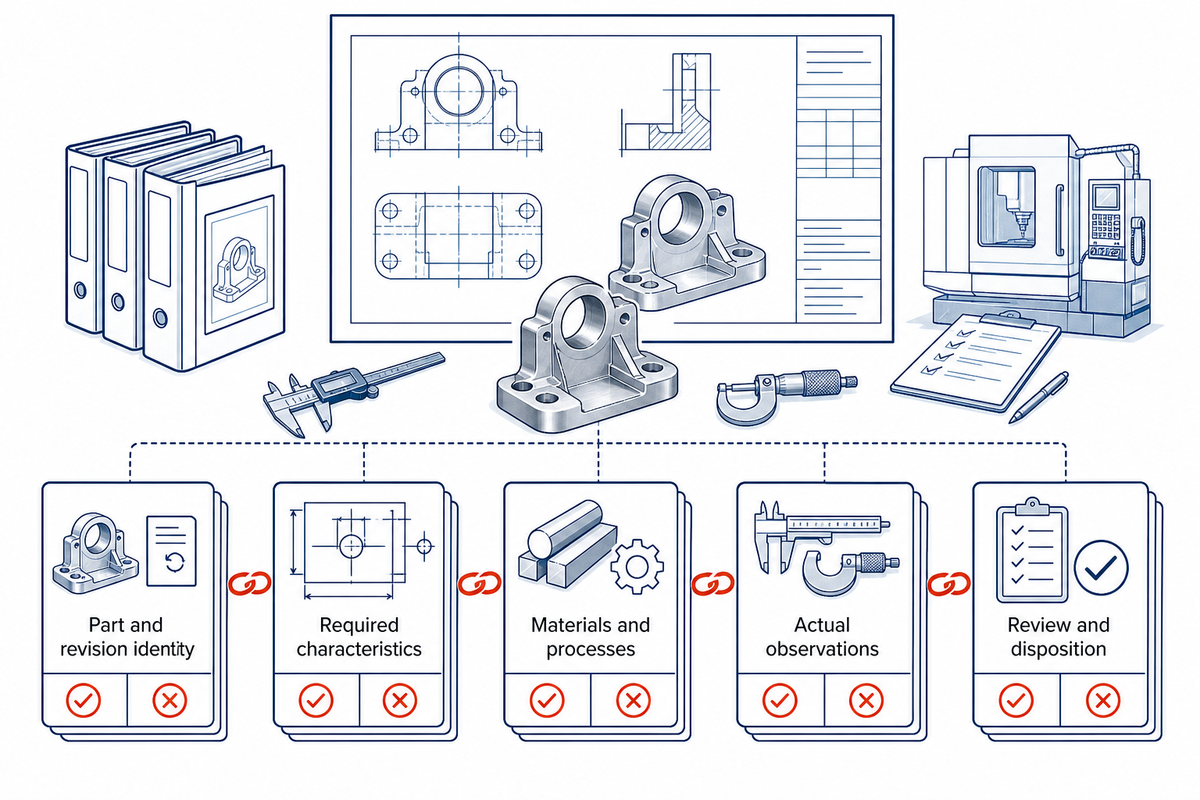
From a quality assurance perspective, a first article inspection is verification activity required by the quality system or contract to demonstrate that specified requirements and characteristics of the product are met. For an inspection report to be acceptable, the evidence and the rationale for acceptance should be clearly documented.
Evidence: SAE AS9102C.
Product identity
Part number, drawing revision, configuration, manufacturing source, and the order or record that controls the review.
Characteristic evidence
The required dimensions, notes, tests, material or process references, actual observations, and acceptance status.
Disposition and approval
Who reviewed the results, how deviations were handled, and whether production or shipment was authorized.
The activity typically happens with a new design or a process change that may affect conformity. Customer procedures may separately address a new supplier, altered manufacturing method, new location, extended downtime, tooling change, and partial re-verification. Do not treat these examples as a universal control-plan list. Verify the trigger wording in the current requirement.
What FAI does not prove
One accepted first article doesn’t prove that every later part will remain conforming. It doesn’t replace process control, tool-wear monitoring, in-process inspection, final inspection, or a customer’s sampling plan. It’s evidence for a defined verification decision at a defined time.
What is first piece inspection?
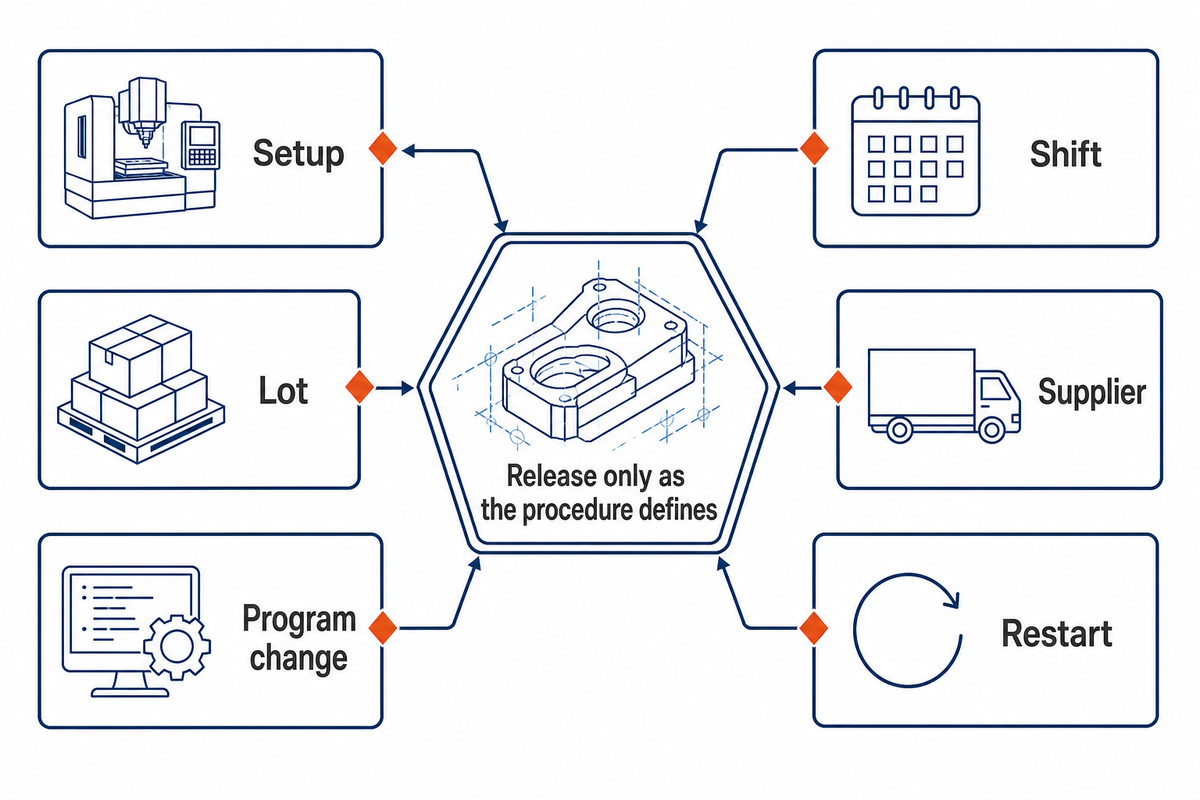
First piece inspection procedures are written to prevent an incorrect setup from producing an entire batch. In production, an inspector or machine operator measures the features named by the procedure and compares each result with the specified value. If there is a difference, the setup is corrected, the required value is recorded, and the check is repeated. Once the required release is obtained, further production may continue.
The terminology trap
Setup release isn’t the only official use of “first piece.” Government evidence also links the term to supplier changes, outsourced builds, per-shift checks, and corrective actions after CNC program changes. Treat setup, shift, lot, supplier, program, and restart as examples; the governing procedure must say which events apply.
A 2024 NIST Manufacturing Extension Partnership case study places first-piece inspection within CNC changeover improvement. The team identified 12 low- or no-cost improvements and reported a 15% increase in milling-department output. That’s useful evidence for a setup-release application, not a cross-industry definition.
A different official use
An NRC incident report traced three out-of-tolerance drill depths to an unauthorized CNC program-code change. The documented corrective action included manager approval for program changes and a first-piece sign-off sheet with 100% inspection on each unit. That coverage belonged to the specific corrective procedure; it shouldn’t be generalized into a universal first-piece rule.
First article vs first piece inspection comparison table
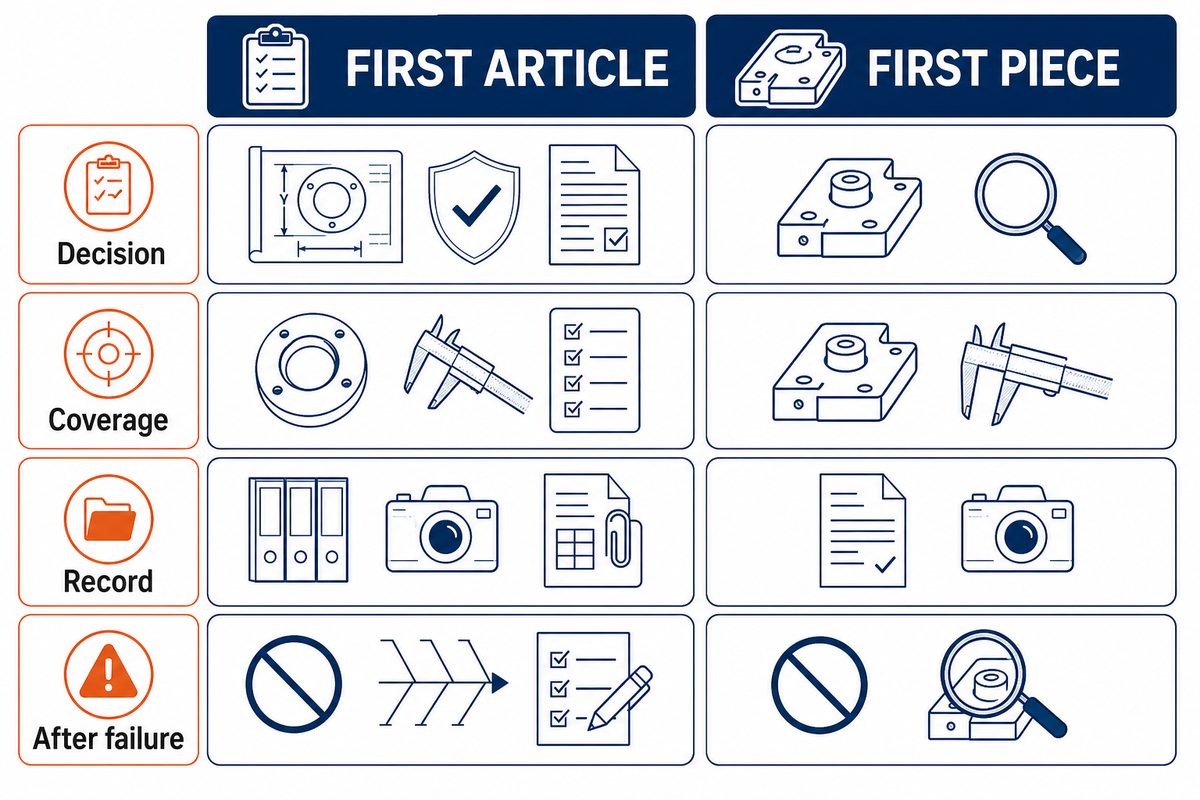
Regime example: FAR Subpart 9.3.
| Question | FAI route | First-piece route | Buyer check |
|---|---|---|---|
| What decision is made? | Whether defined product-verification evidence is acceptable | Whether the named production event may proceed | State the release decision explicitly |
| What is measured? | The characteristics required by the governing FAI scope | The characteristics required by the first-piece plan | Never infer coverage from the label |
| What is recorded? | Revision-controlled results and required supporting records | Event identity, measured values, result, and release sign-off | Require actual values where the plan calls for them |
| What happens after failure? | Contain, correct, document, and obtain the required disposition | Hold the run, correct the cause, and repeat the defined release check | Name the authority before production starts |
| What follows approval? | Production under the approved process and control plan | Continued production with specified in-process controls | Approval is not permission to stop monitoring |
The examples in the table depict common operating patterns and should not replace a customer quality manual. One purchaser may expect a complete first-piece inspection, while another may request a limited check. The buyer and supplier should align customer expectations with the inspection intent before quoting or production.
When is each inspection required?
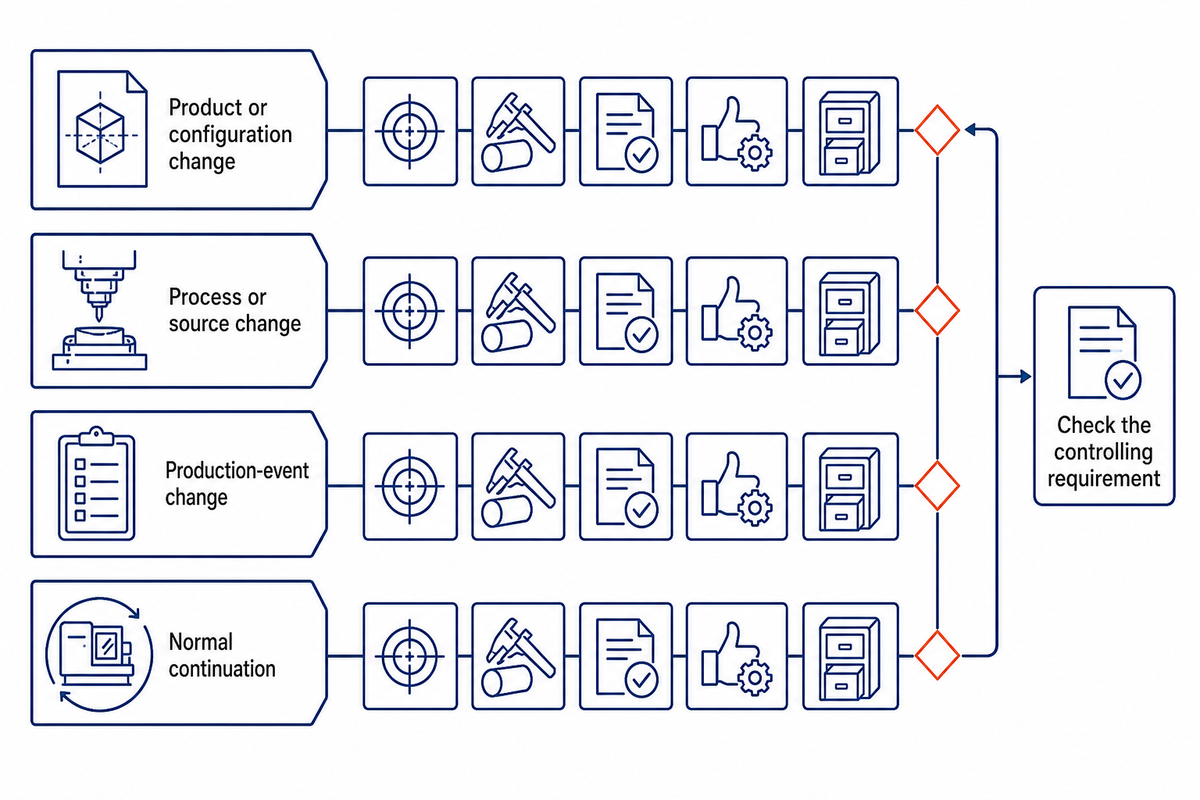
Events must be classified with the Change Trigger Ladder and a first article inspection checklist before selecting the record. The ladder does not decide the answer; it exposes which customer, contract, drawing, or control-plan requirement must govern the trigger, characteristic coverage, and record depth.
Trigger example: FAR Subpart 9.3.
- Product or configuration change: new part number, drawing revision, material, or specified characteristic.
- Process or source change: manufacturing method, location, supplier, special process, tooling strategy, or other customer-defined change.
- Production-event change: machine setup, fixture, tool, offset, CNC program, shift, batch, lot, or restart.
- Normal continuation: production remains within the same approved state and follows its established in-process and final controls.
Ask for FAI evidence when
The controlling requirement calls for documented product verification after a new or changed condition, or for a partial/full re-verification.
Ask for first-piece evidence when
The applicable procedure defines an event that must be released before the remaining quantity may proceed.
The controls can overlap. A first-piece inspection may protect the shop against a setup error, while an FAI package may satisfy a customer review. In-process inspection may also be required to detect drift during the run. Each control serves a different function and answers a different question.
What records should each inspection produce?
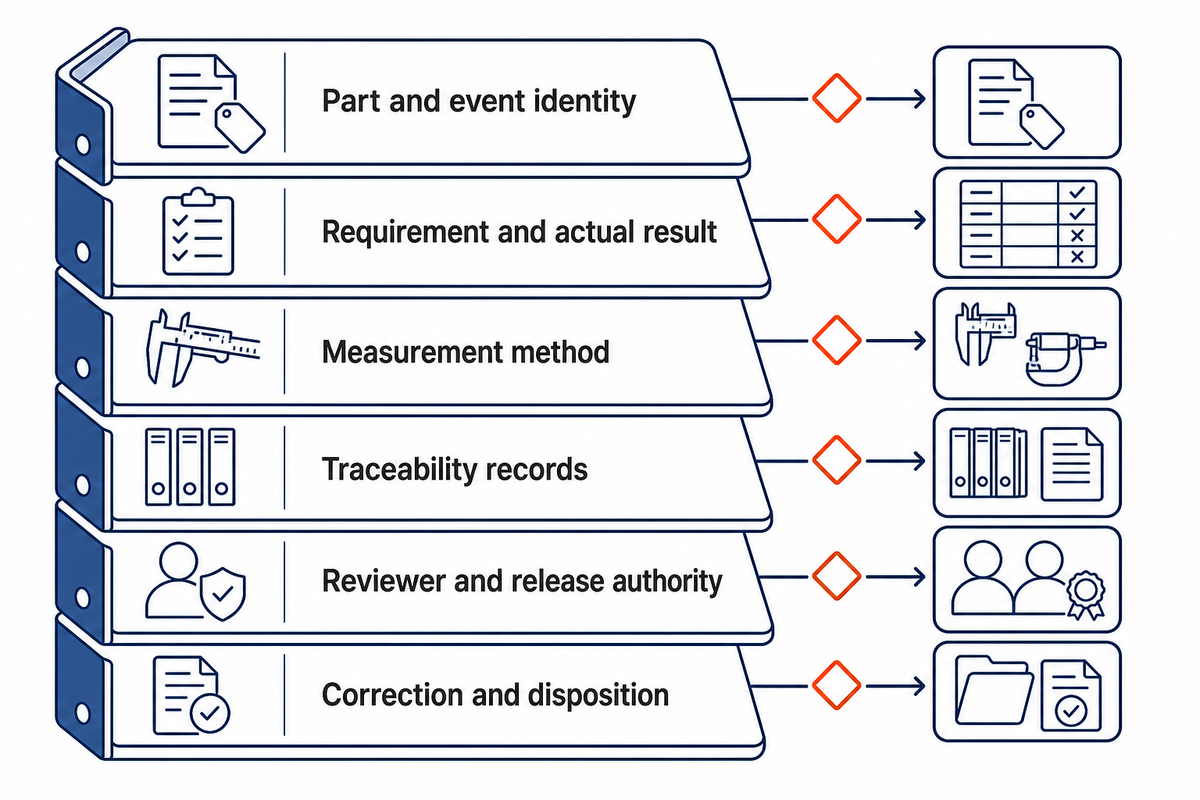
Use the Record Depth Test. Would a reviewer understand what was performed, what was observed, what production and revision events were affected, who approved the outcome, and how deviations, if any, were handled? If the answer is no, then the “pass” stamp doesn’t establish an acceptable evidence trail.
Record reference: SAE AS9102C.
Buyer-ready record fields
- Part number, drawing/specification revision, order, lot or event identity
- Characteristic identifier, requirement, actual measured result, and units
- Measurement method or equipment reference where required
- Material, process, and traceability records required by the order
- Inspector/reviewer identity, date, acceptance status, and release authority
- Nonconformance, correction, recheck, and customer disposition status
The following example shows a record syntax. It isn’t a Zhenling product specification or acceptance plan. It demonstrates that a numeric requirement, along with a result and a unit, is a lot more informative than a simple “pass.” Characteristics, limits, as well as measurement and rounding methods shown in the buyer’s drawing and the inspection procedure must be specified to fully describe a measurement.
Before agreeing on that record format, buyers should compare the part’s controlled characteristics with the supplier’s metrology resources and inspection methods.
| Data type | Illustrative requirement entry | Illustrative actual-value entry |
|---|---|---|
| Diameter | 25.000 mm | 24.998 mm |
| Position | 0.050 mm | 0.038 mm |
| Flatness | 0.030 mm | 0.021 mm |
| Surface roughness | 1.6 μm | 1.4 μm |
| Angle | 90.0° | 89.9° |
| Pressure | 10.0 bar | 10.1 bar |
| Temperature | 20.0 °C | 20.4 °C |
| Rotational speed | 1000 rpm | 998 rpm |
| Frequency | 50 Hz | 49.9 Hz |
| Voltage | 24 V | 23.9 V |
This is a procurement checklist, not a general form. An archived JPL clause, for example, required AS9102-based FAI and 100% recording of design characteristics, allowable tolerances, actual values, test information, and quality acceptance. That shows how deep one contract can go; it doesn’t authorize copying its historical requirements into another customer’s order.
Avoid “pass-only” evidence
Actual values help reveal margin, repeat errors, gauge issues, and process drift that a pass/fail checkbox hides. When the controlling requirement allows attribute recording, retain enough context to show what was checked and which acceptance rule was used.
How to write a usable inspection plan
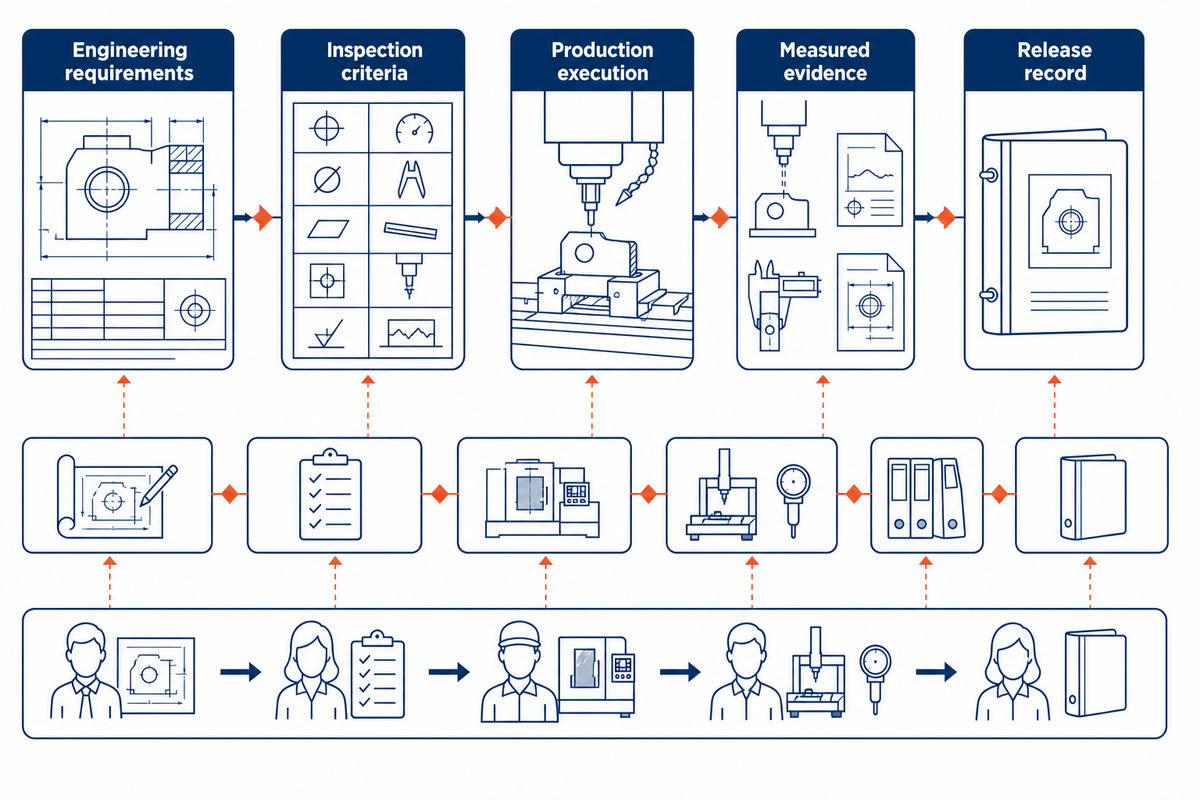
Good quality assurance planning gives engineering, manufacturing, and quality control different but connected responsibilities. Engineering identifies drawing and customer requirements; the QA process translates them into inspection criteria; the manufacturer executes the production process; and the release owner preserves the assurance record. That chain is designed to catch a defect early, reduce downstream risk, and show conformance without assuming that every inspection has the same scope.
Case evidence: NRC corrective-action report.
Plan fields that prevent ambiguity
- State the acceptance criterion, required accuracy, measurement orientation, and method for each characteristic requiring inspection.
- Separate incoming checks, first-piece release, detailed inspection, in-process control, and final acceptance.
- Define whether a nonconforming result will reject the unit, hold the full batch, or trigger an authorized review.
- Name the sample size, the authorization needed to resume, and the person who may approve a deviation.
- Identify the record used to track status, whether that’s a controlled form or a quality module within an ERP system.
Digital indicators and real-time alerts can speed the response, but software does not choose the acceptance rule. The team still has to inspect against the controlled requirement, analyze the result, and decide whether the evidence supports validation or release. If the method, program, or drawing is out of date, faster data collection only produces a faster wrong answer.
A proactive, systematic methodology supports reliability in high-volume or continuous production across the product lifecycle. When quality issues recur, reliable processes investigate the root cause and the leading cause of escape, then document the review and data. Continuous improvement efforts standardize review steps while focusing on product risks. Customer and order documents define the requirements; organizational authority tailors the plan and identifies the release owner. Useful standardization is adapted to process control, but never overrides the customer contract.
Where AS9102 fits, and where it does not
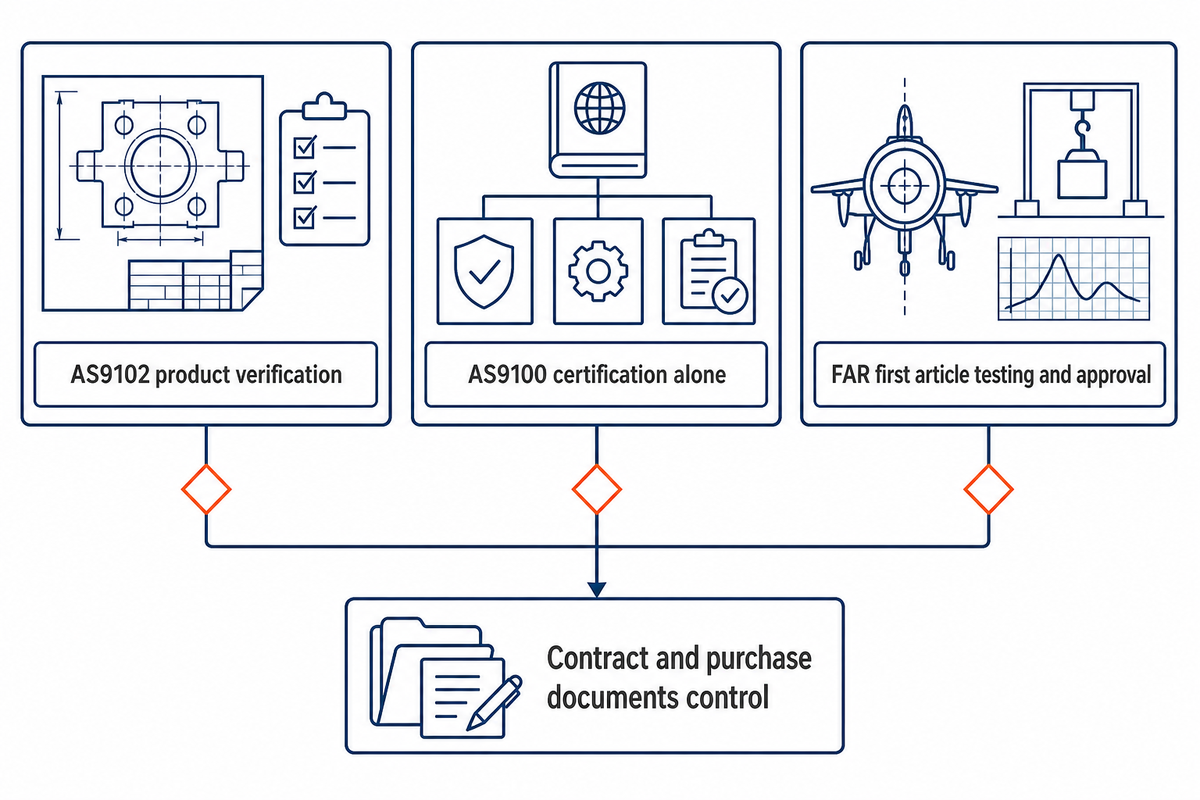
The official SAE AS9102C record identifies the 2023 revision as “Aerospace Series, First Article Inspection Requirements.” IAQG describes 9102 as consistent process and documentation requirements for verification of aviation, space, and defense product. That product-verification language is more precise than calling every FAI a broad “process qualification.”
| Statement | Safe conclusion |
|---|---|
| A supplier is AS9100 certified | That alone does not establish that every order requires an AS9102 report |
| The contract flows down AS9102C | Use the current licensed requirements plus customer-specific instructions |
| A company voluntarily adopts AS9102 | Document the chosen scope and do not imply customer approval that was not granted |
| A work instruction says “first piece” | Do not assume AS9102 forms or full FAI coverage unless the requirement says so |
IAQG implementation guidance states that 9102 may be required by contract or self-imposed and is not required by another published standard. This is why “AS9100 certified” should never be translated automatically into “AS9102 required.” The customer’s current flow-down and purchase documents still control.
There is a second terminology distinction in U.S. procurement. FAR Subpart 9.3 uses “first article testing and approval” for a contract-defined regime that can cover a preproduction model, initial production sample, test sample, first lot, or pilot lot. The solicitation states the characteristics, tests, and report data; that isn’t automatically the same deliverable as an AS9102 FAIR.
CNC machining example: setup release and documented product verification
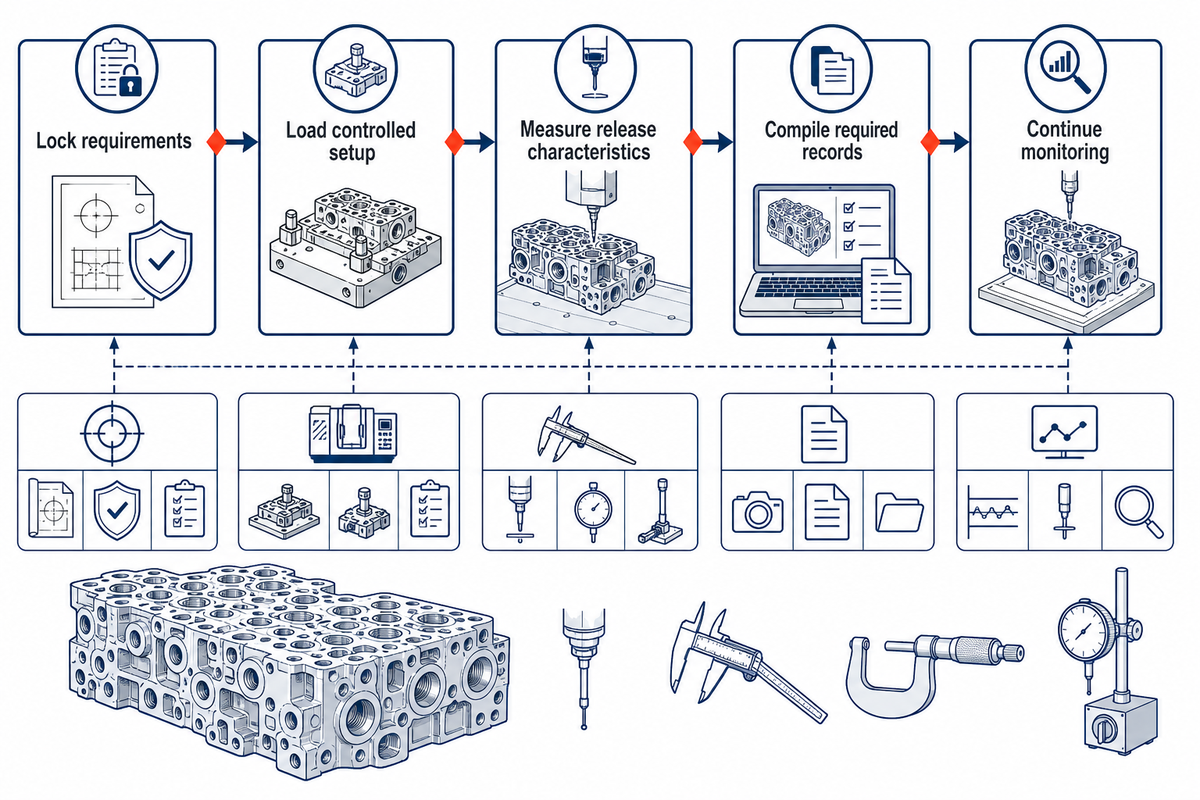
Consider a hypothetical custom-machined valve body. The drawing and order identify the revision and inspection requirements, but no tolerance, measurement result, or acceptance limit is invented here. The manufacturing team reviews the drawing, prepares the CNC program and fixture, selects measurement methods, and produces an initial part.
Case evidence: NIST MEP CNC changeover study.
1. Review
Lock the part, revision, notes, material, process, and customer clauses.
2. Set up
Load the program, tools, fixture, work offset, and inspection plan.
3. Check first piece
Measure the defined release characteristics and hold the run until accepted.
4. Complete FAI
When required, compile the broader characteristic and supporting record package.
5. Control the run
Continue the specified in-process monitoring, tool control, and final release.
If the first piece fails, the team contains production and identifies the cause. It then corrects the program, tool, offset, fixture, or measurement method as appropriate and repeats the required check. If the order requires FAI, the supplier completes that evidence only after the product state is ready for verification. A buyer can review Zhenling Metal’s metrology and inspection capabilities when aligning the measurement plan for a custom part.
Supplier context can also shape audit depth. Zhenling Metal’s factory covers 8,000 m², including a 6,000 m² workshop, so the workshop occupies 75% of the site footprint; the company also reports that 80% of its products are exported. These scale figures do not define inspection requirements, but they can help buyers frame capacity and traceability questions.
One part, two decisions
The same physical unit may be used for the first-piece release and the FAI record when the governing procedure allows it. Equivalence comes from completing every required characteristic, record, traceability item, and approval, not from using the same serial number.
Common mistakes that create false confidence
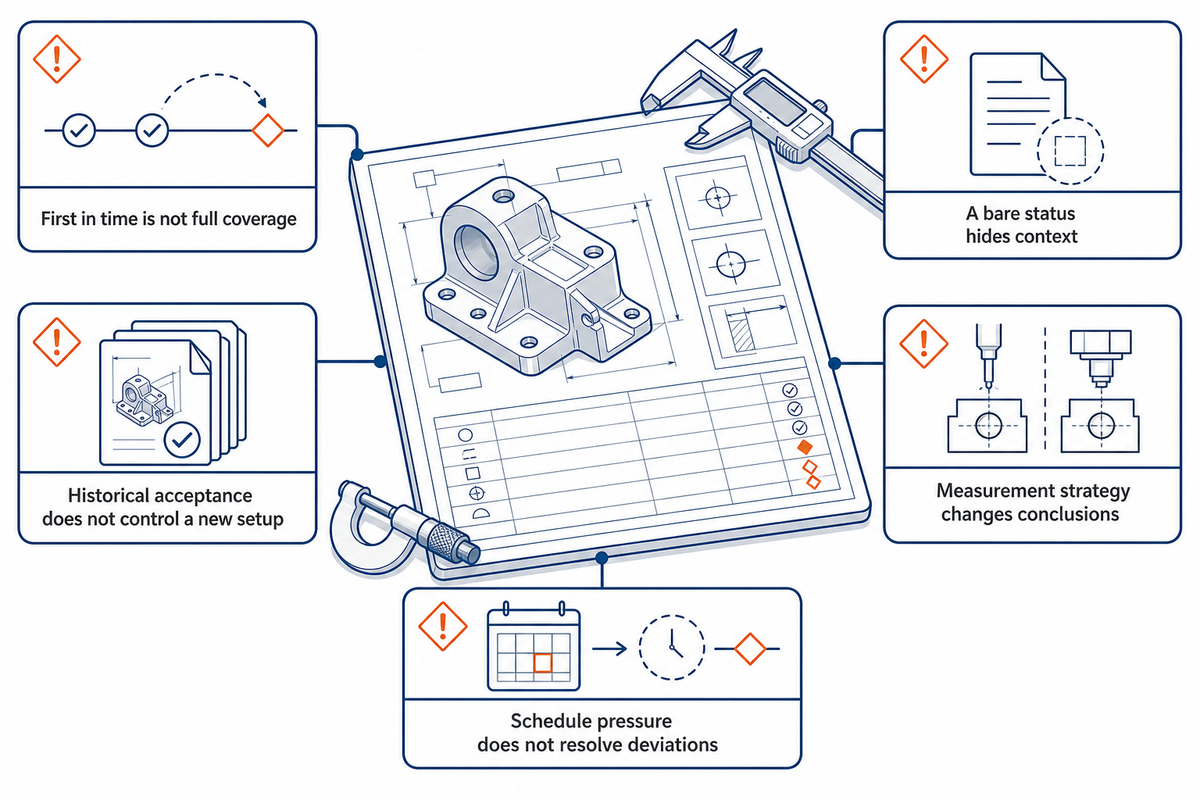
Mistake evidence: NRC CNC program-change report.
Mistake 1: the first part equals a full FAI
Chronology doesn’t prove coverage. Check the required characteristics, supporting records, and approval path.
Mistake 2: an earlier FAI clears every later setup
A conforming historical package doesn’t prevent a new offset, tool, fixture, program, or loading error.
Mistake 3: “pass” is enough
A bare status hides the revision, actual value, equipment context, approver, and unresolved deviation.
Mistake 4: the gauge decides the truth
Measurement strategy, datum setup, restraint condition, calibration status, resolution, and operator method can change the conclusion.
Schedule pressure can leave deviations unresolved and push product toward shipment even when requirements are not met. Performing an inspection does not make a nonconforming result acceptable. The defined containment, review, concession, rework, and re-inspection process must be completed before release.
Decision framework: the 6-question Release Scope Gate
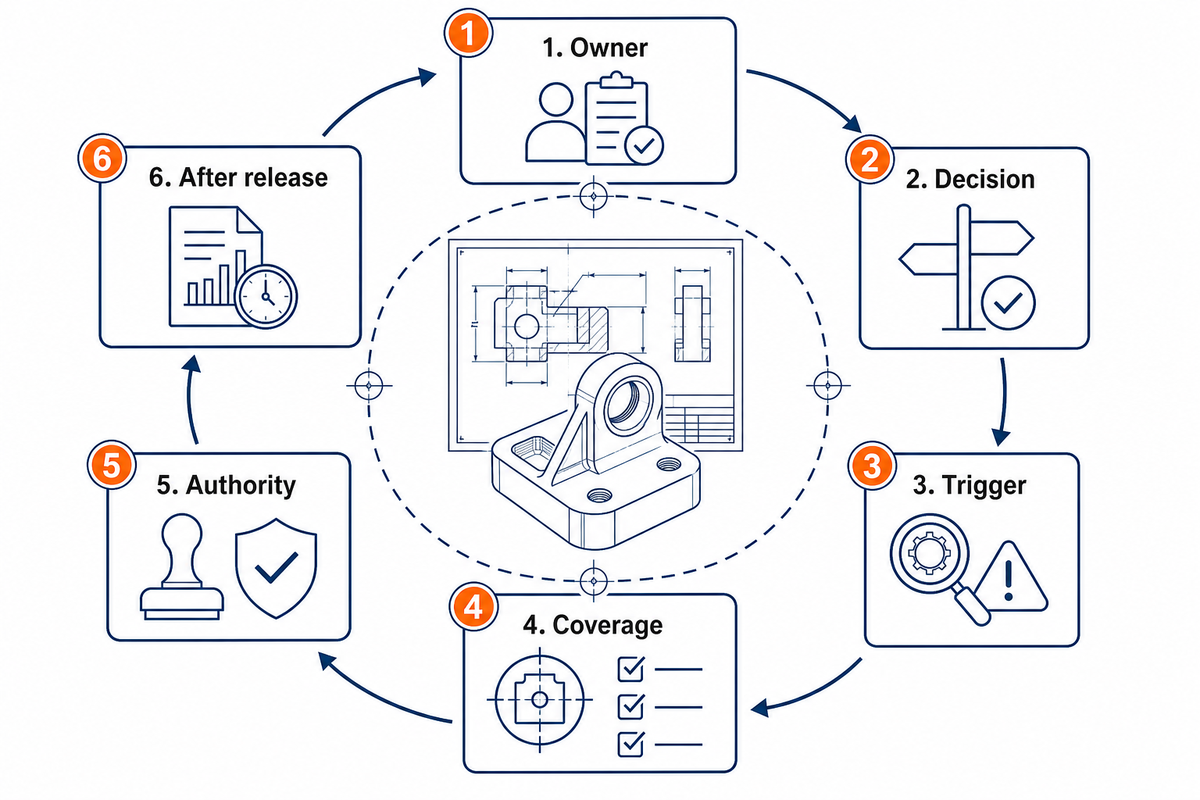
The Release Scope Gate transforms vague language into a set of six auditable questions. These questions can be answered prior to obtaining a supplier’s quote or selecting a report template.
Procurement example: FAR Subpart 9.3.
- Owner: which contract, drawing, standard, customer clause, control plan, or work instruction controls?
- Decision: are you verifying specified product evidence, releasing a production event, approving a federal first article test, or making another decision?
- Trigger: what changed, and does the requirement call for a new, full, partial, or event-specific inspection?
- Coverage: which characteristics, tests, materials, processes, and records must be included?
- Authority: who may accept the result, and who may disposition a deviation?
- After release: which in-process, tool-control, sampling, final-inspection, and retention rules continue?
Define the inspection deliverable before machining starts
Share the drawing revision, order requirements, characteristic coverage, report format, approval owner, and change triggers. Zhenling Metal can align the manufacturing and measurement plan with your defined requirements without turning a shorthand label into an unsupported promise.
Frequently asked questions
Is first piece inspection the same as first article inspection?
Not necessarily. Many machine shops use first piece inspection as a setup-release check and first article inspection as broader documented product verification, but official and contractual usage isn’t uniform. First-piece controls can also be tied to a shift, lot, supplier, program change, or outsourced build. The drawing, purchase order, customer quality clause, control plan, contract, and applicable standard must define the actual decision and evidence.
Does AS9100 require a first article inspection?
No, not by certification alone. IAQG guidance says AS9102 may be contractually required or voluntarily adopted and isn’t required by another published standard. An AS9100-certified supplier should therefore review the current contract, customer-specific flow-downs, product history, and applicable requirement before deciding whether a new, full, or partial AS9102 FAI is needed. Don’t infer the deliverable from the certification name.
When should a first piece inspection be repeated?
Repeat it when the applicable procedure names an event that could change conformity. Common examples include a new setup, tool or insert change, fixture change, CNC program or offset adjustment, restart, shift, batch, lot, supplier, or material transition. These are examples rather than universal triggers. The control plan or customer procedure should define what must be rechecked, who releases the work, and which in-process controls remain after approval.
Can one part serve as both the first piece and the first article?
Yes, when the governing procedure permits it and the records satisfy both scopes. Sharing one physical unit doesn’t make a setup check equivalent to a complete FAI.
Is first article testing and approval the same as an AS9102 FAI?
No. U.S. federal procurement can use “first article testing and approval” for a contract-defined evaluation of a preproduction model, initial production sample, test sample, first lot, or pilot lot, followed by written contracting-officer approval. FAR Subpart 9.3 places the required characteristics, tests, and approval route in the solicitation and contract. AS9102, by contrast, is an aerospace first article inspection requirement focused on documented product verification. A federal contract could invoke its own first article testing clause, flow down AS9102, require both, or require neither; the shared words don’t merge the deliverables. Buyers should identify the controlling clause, report data, approving authority, and resubmission triggers in the order.
What should a buyer request from a CNC supplier?
Start with the governing drawing revision, purchase-order clauses, and the exact release decision. Then state which characteristics require actual values, which can use attribute results, which material or special-process records must accompany the report, and whether the supplier must use a customer form. Identify first-piece, sampling, in-process, and final-inspection rules separately so approval of one record isn’t mistaken for release from the others.
Also name the trigger for a full or partial repeat, the person authorized to approve results, the path for concessions, and the required retention and delivery format. If AS9102C, a federal first article clause, or a customer-specific portal is required, cite it explicitly. This gives the supplier enough information to plan measurement methods, inspection time, and document control before production rather than discovering an unquoted reporting package after machining.
Conclusion
In making the determination of first piece or first article inspection, relying on a label is a failure to define the requirement. Other considerations, including the controlling document, change trigger, characteristic coverage, record depth, evidence, approval owner, and continuing controls, remain to be defined. This discipline protects the customer and supplier from agreeing on language while expecting different evidence.
References & sources
- SAE AS9102C official standard record
- IAQG 9102 First Article Inspection Requirement resources
- NIST MEP first-piece inspection and CNC changeover case study
- NRC CNC program-change and first-piece corrective-action report
- BSI catalog record for SAE AS9102C:2023
- FAR Subpart 9.3: first article testing and approval